

What Is MIM Molding?
MIM molding (Metal Injection Molding molding) is an advanced manufacturing process that combines plastic injection molding technology with powder metallurgy to produce complex metal components with high precision and excellent mechanical properties.
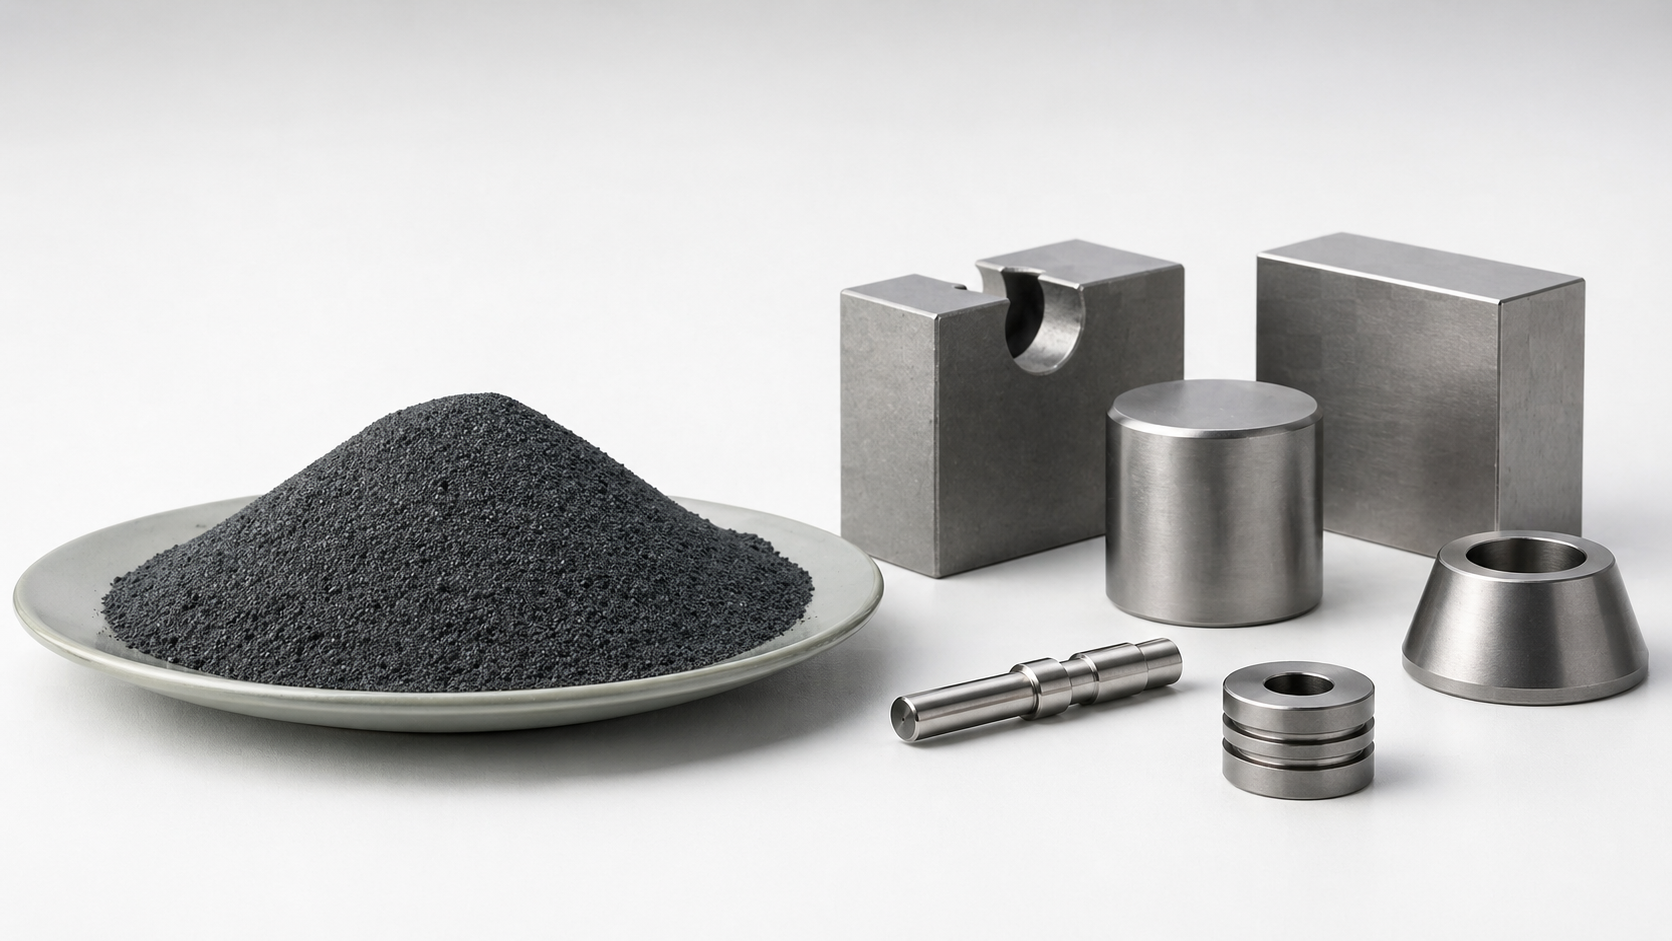
Unlike traditional CNC machining, which removes material from a solid block, MIM molding uses metal powder mixed with a polymer binder to create a feedstock that can be injected into molds. After molding, the binder is removed, and the parts are sintered at high temperatures to achieve final density and strength.
This process is especially suitable for producing small, complex metal parts in medium to high volumes, where traditional machining may become costly or inefficient.

How Does MIM Molding Work?
The MIM molding process consists of four major stages:
1. Feedstock Preparation
Fine metal powders are mixed with thermoplastic binders to create a homogeneous MIM feedstock.
Common materials include:
- Stainless steel 304 / 316L
- 17-4PH stainless steel
- Tool steel
- Titanium alloys
- Nickel alloys
- Copper alloys
The powder size and binder system directly affect molding performance, dimensional accuracy, and final mechanical properties.
2. Injection Molding
During the molding stage, the MIM feedstock is heated and injected into a precision mold under controlled pressure.
Similar to plastic injection molding, this step allows manufacturers to produce:
- Thin walls
- Complex geometries
- Internal channels
- Micro features
- Multiple functional details
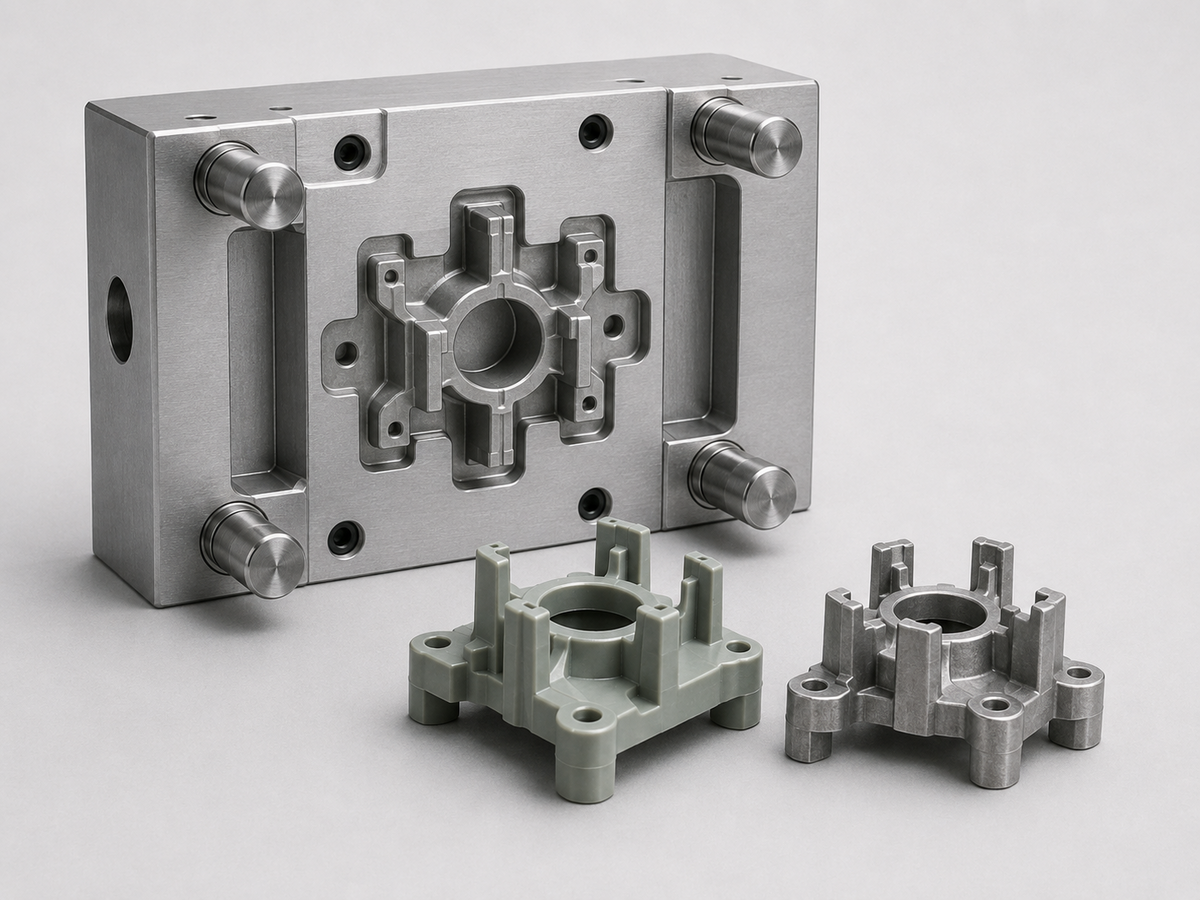
The molded component is called a "green part" because it still contains polymer binders.
3. Debinding
The binder removal process eliminates polymer materials from the molded part while maintaining the original shape.
Depending on the material system, debinding can include:
- Solvent debinding
- Thermal debinding
- Catalytic debinding
Proper debinding control is critical because defects during this stage can lead to cracks, distortion, or incomplete sintering.
4. Sintering
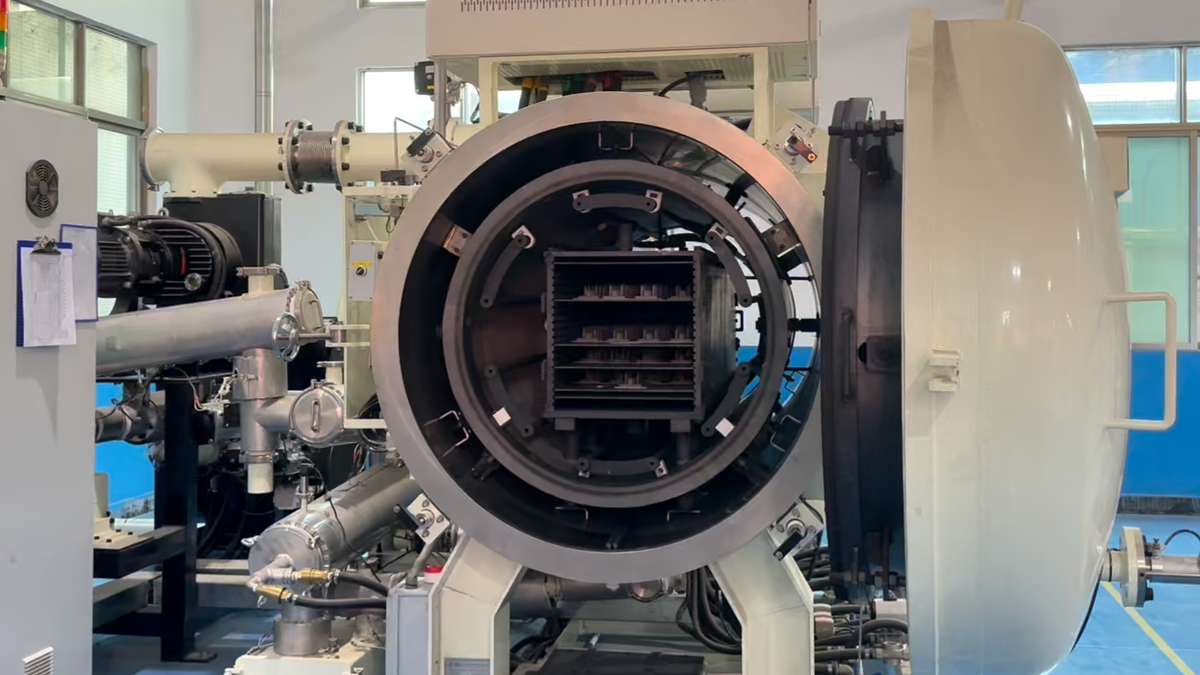
After debinding, the parts are heated in a controlled atmosphere furnace.
During sintering:
- The metal particles bond together
- The part shrinks approximately 15–25%
- Density and mechanical strength increase
Advanced MIM molding technology can achieve final densities above 95% of theoretical density, providing properties close to traditional metal manufacturing methods.

Advantages of MIM Molding
1. Complex Metal Parts Without Extensive Machining
One of the biggest advantages of MIM molding is the ability to manufacture highly complex metal components in a single molding process.
Features such as:
- Undercuts
- Small holes
- Thin ribs
- Curved structures
- Internal cavities
can often be produced without additional machining operations.
This makes MIM ideal for applications where component miniaturization and functional integration are required.
2. High Production Efficiency
For high-volume production, metal injection molding can significantly reduce manufacturing costs compared with CNC machining.
After mold development, MIM production offers:
- Stable cycle times
- Consistent part quality
- Reduced material waste
- Automated production capability
It is commonly used for thousands or millions of identical components.
3. Excellent Surface Finish
MIM molded parts typically achieve smooth surface finishes directly after sintering.
Typical surface roughness:
- Ra 1–3 μm (depending on material and process conditions)
Additional finishing processes can include:
- Polishing
- Electroplating
- PVD coating
- Passivation
- Heat treatment

4. Wide Material Selection
A major benefit of MIM molding is its compatibility with many engineering metals.
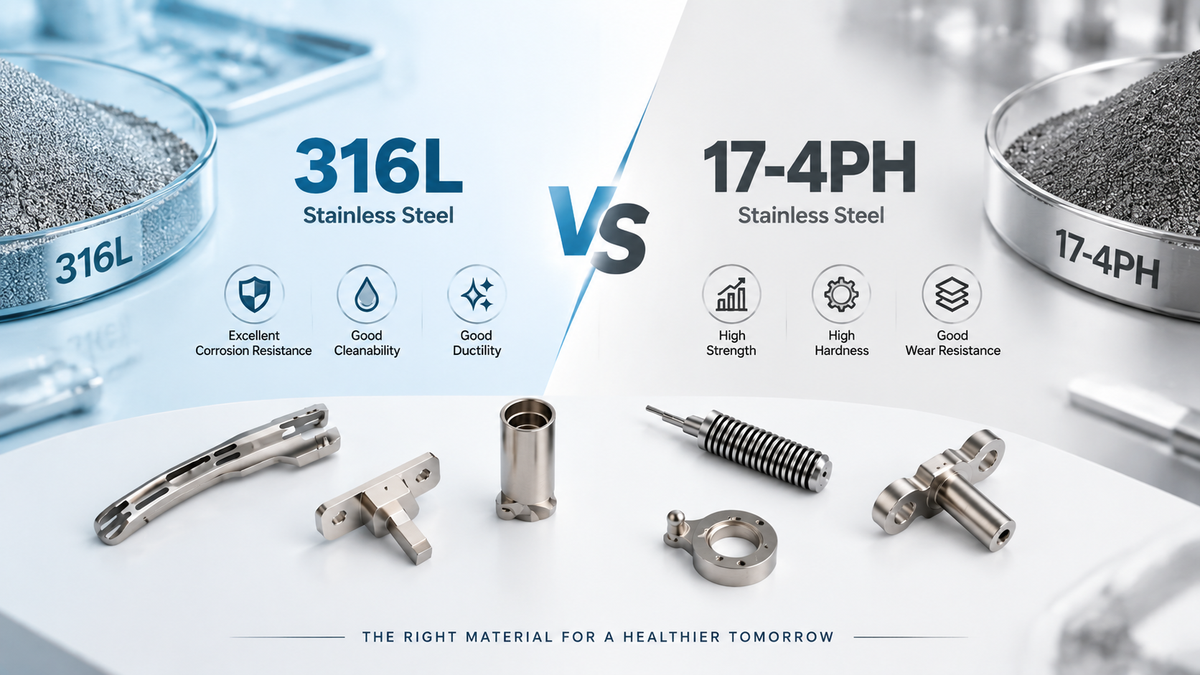
| Material | Typical Applications |
|---|---|
| 316L Stainless Steel | Medical devices, chemical equipment |
| 17-4PH Stainless Steel | Aerospace, industrial components |
| Titanium | Medical implants, lightweight parts |
| Nickel Alloy | High-temperature applications |
| Copper Alloy | Electrical components |
Material selection depends on strength, corrosion resistance, conductivity, and operating environment.
Design Considerations for MIM Molding
Successful MIM production requires early design evaluation.
Wall Thickness
Uniform wall thickness helps prevent:
- Sink marks
- Cracking
- Uneven shrinkage
Typical MIM wall thickness:
- 0.3–3 mm for many applications
Very thin sections require careful material and mold design.
Shrinkage Compensation
Because MIM parts shrink during sintering, mold dimensions must compensate for predictable shrinkage.
Factors affecting shrinkage include:
- Material composition
- Powder loading
- Part geometry
- Sintering conditions
Professional MIM manufacturers use simulation and process validation to control dimensional accuracy.
Tolerance Requirements
Standard MIM tolerances are typically around:
- ±0.3% of dimension
Tighter tolerances may require:
- Secondary machining
- Grinding
- Precision finishing
Critical dimensions should be identified during DFM review.
Applications of MIM Molding
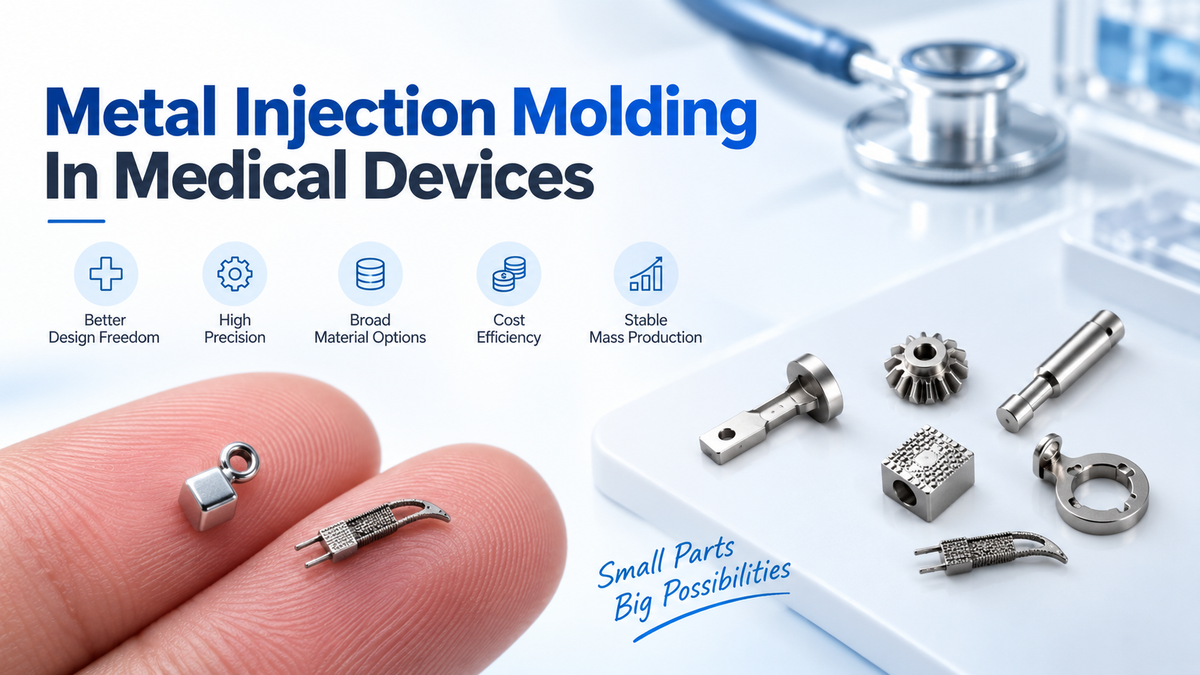
Medical Devices
MIM molding is widely used for:
- Surgical instruments
- Orthopedic components
- Medical housings
- Dental tools
Stainless steel MIM materials provide corrosion resistance and sterilization capability.
Consumer Electronics
Miniaturized electronic products require lightweight and precise metal components.
Typical applications:
- Hinges
- Brackets
- Connectors
- Structural parts

Automotive Components
MIM components are used in:
- Sensor parts
- Locking mechanisms
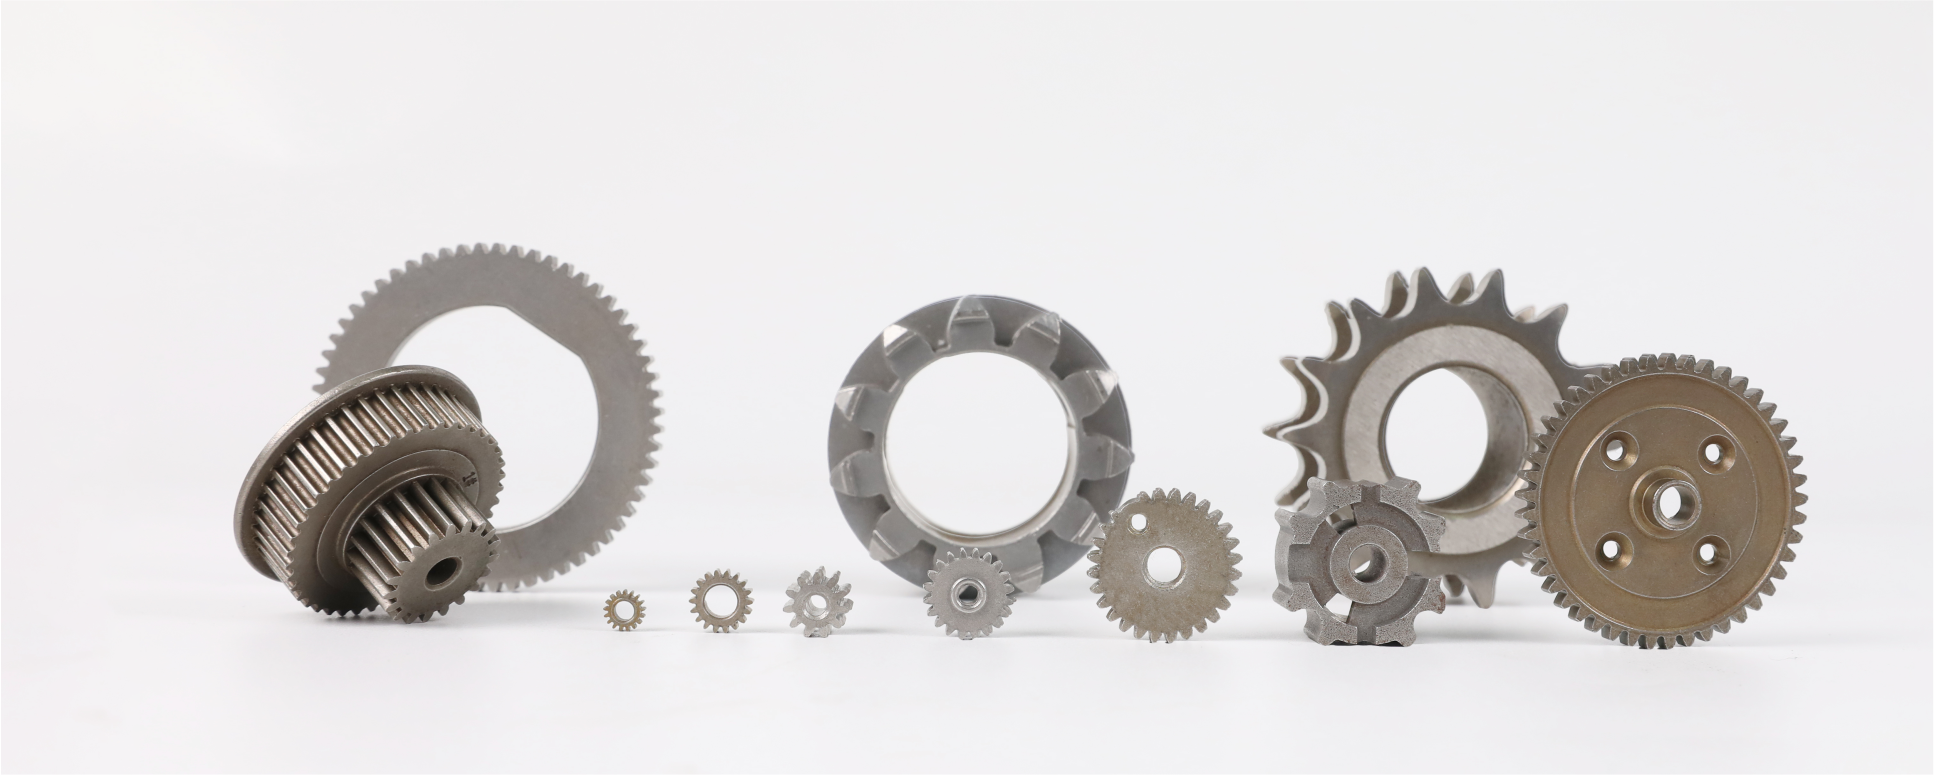
- Gear components
- Actuator parts
The process supports high-volume production with consistent quality.
Robotics and Industrial Equipment
As robotic systems become smaller and more precise, MIM molding helps manufacture compact metal components with complex geometries.
Applications include:
- Micro gears
- Robot joints
- Precision brackets
- Functional connectors

Why Choose XY-Global for MIM Molding?
XY-Global provides integrated MIM molding solutions from prototype development to mass production.
Our capabilities include:
- Metal Injection Molding (MIM)
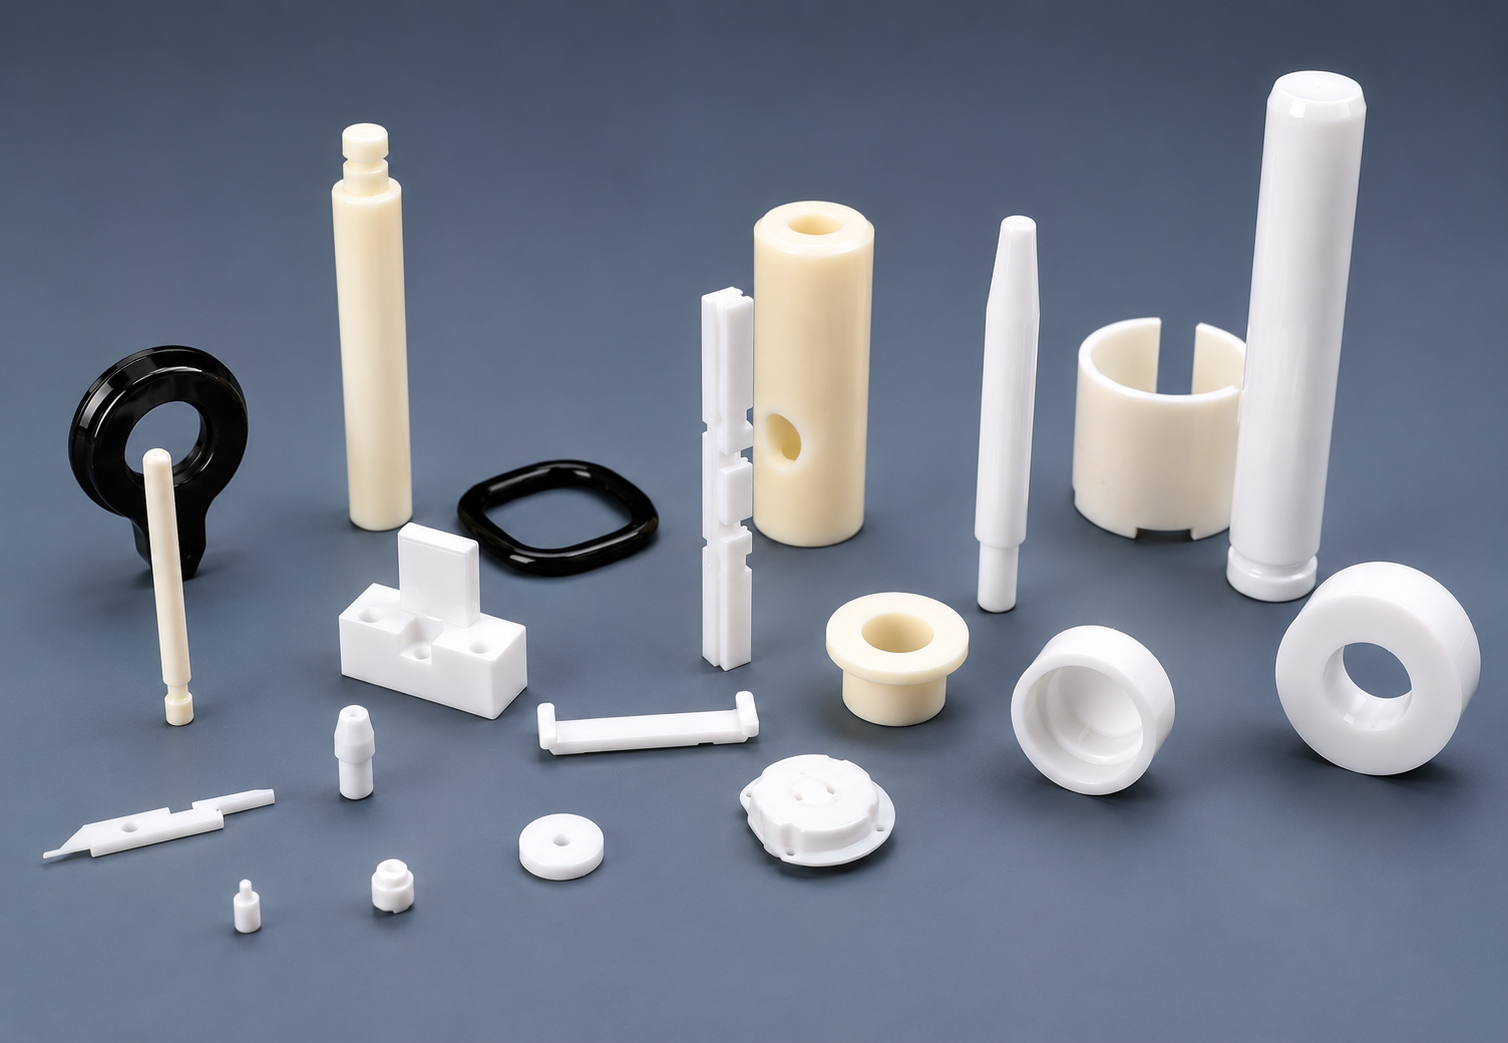
- Ceramic Injection Molding (CIM)
- CNC machining
- Surface treatment
- Precision inspection
- Assembly services
With ISO9001 and ISO13485 certified manufacturing systems, we support customers from early design validation to stable production.
Our engineering team provides:
- DFM analysis
- Material selection support
- Mold design optimization
- Process validation
- Quality inspection reports
Whether you need micro metal components or complex MIM parts for industrial applications, we help transform designs into reliable production solutions.
FAQ
What metals can be used in MIM molding?
Common materials include stainless steel, titanium, nickel alloys, copper alloys, and tool steels.
Is MIM molding suitable for prototypes?
MIM is usually more suitable for medium and high-volume production. For prototypes, CNC machining or 3D printing may be more economical before moving to MIM production.
What is the typical size range of MIM parts?
MIM is mainly used for small precision components, typically from several millimeters to around 100 mm depending on geometry and material.
How accurate are MIM molded parts?
Typical MIM accuracy is around ±0.3% of dimension. Higher precision can be achieved through secondary machining processes.
What is the difference between MIM molding and plastic injection molding?
Plastic injection molding produces polymer parts, while MIM molding uses metal powders combined with binders to create final metal components after debinding and sintering.
Conclusion
MIM molding provides an efficient solution for manufacturing small, complex metal components that require high precision, repeatability, and production efficiency.
By combining injection molding flexibility with metal material performance, MIM has become an important technology for medical, automotive, electronics, robotics, and industrial applications.
For companies looking for reliable MIM manufacturing solutions, early DFM evaluation and process planning are key factors for achieving successful mass production.
Contact XY-Global to discuss your MIM molding project and explore the right manufacturing solution for your metal components.
Share:
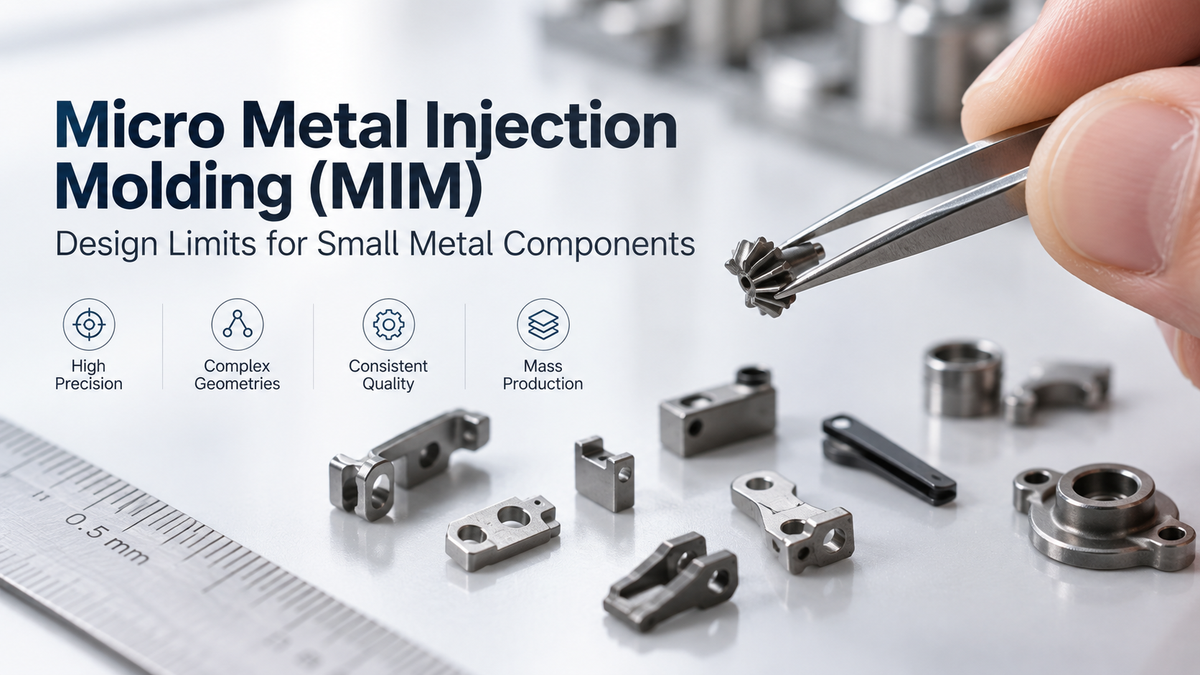
Micro Metal Injection Molding (MIM) Design Limits for Small Metal Components